


Computer Vision for Manufacturing
A missed defect that reaches your customer costs far more than the inspection that would have caught it. DAC.digital designs and builds custom computer vision systems for manufacturers who need consistent quality control, faster defect detection and safer production lines, without stopping the line to get there.

23 Deloitte Fast 50 Central Europe 2023
Deloitte Fast 50
Forbes Technology Council Official Member
Forbes
1000 Europe’s Fastest Growing Companies
2023 & 2024
Financial Times
Polish Company International Champion 2020
PwC
Master of Innovative Transformation 2021
MIT Sloan Review
What computer vision solves on your production line

Quality control
Defect detection, assembly verification, foreign object detection and dimensional checks: the most common use of computer vision in manufacturing, with high-resolution cameras detecting surface imperfections in metal, plastic, glass and composite materials before they slip past a human inspector. DAC.digital systems have caught defects down to a fraction of a millimetre, for example 250 microns in our 10beauty precision-robotics project. Read more about automated quality control →

Safety and monitoring
Real-time monitoring of PPE compliance, restricted-zone entry and unsafe behaviour on the factory floor, including posture detection that helps prevent injuries during manual material handling, so hazards get flagged before they cause an incident. In 2020, 4,764 U.S. workers died from workplace injuries, according to the Bureau of Labor Statistics, with material handling, transportation and heavy machinery among the leading causes, exactly the kind of conditions vision-based safety monitoring is built to catch in real time.

Object identification
Using image recognition to read barcodes, serial numbers and labels, and recognising unlabelled parts by their own features, to identify and sort products on the line. Computer vision also verifies that products are correctly labelled and packaged before shipment. Read more about object identification →
Robotics and automation
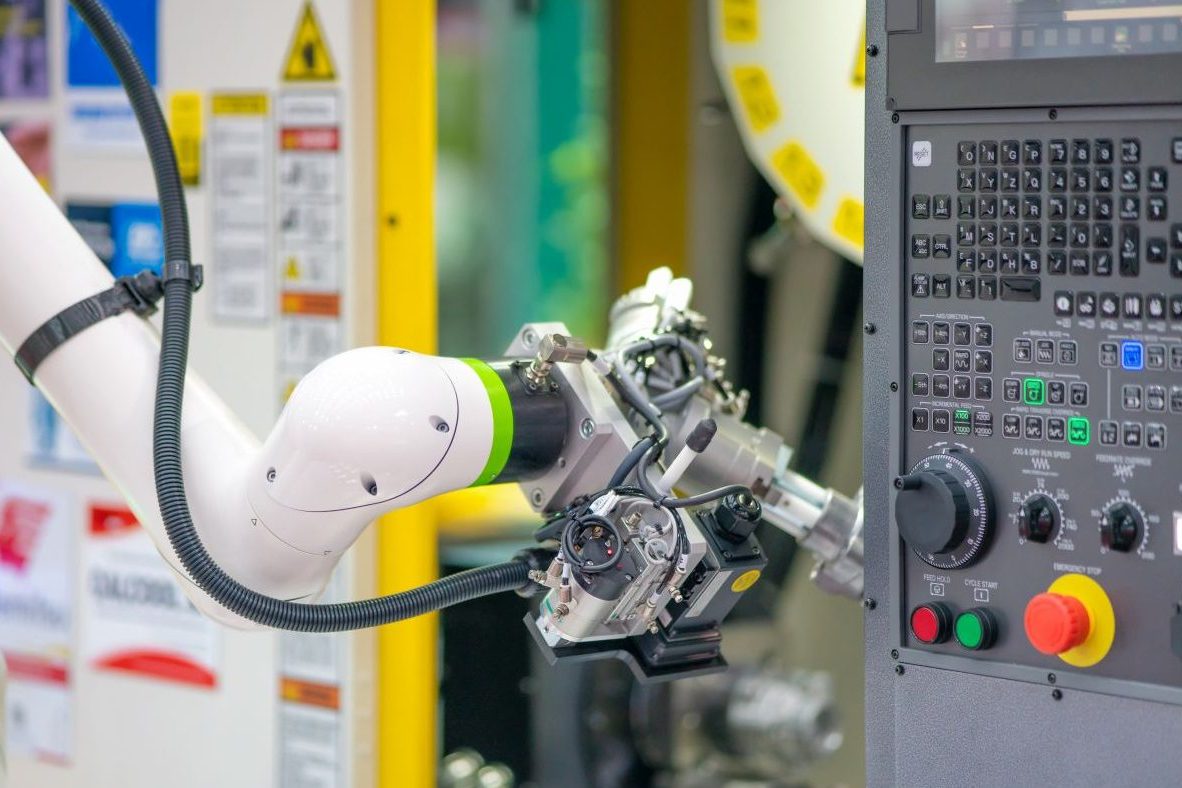
Vision-guided pick-and-place and precision assembly that lets robots and cobots handle variable parts, not just fixed positions.
Proven on real production lines
Three examples of computer vision systems DAC.digital has built for manufacturers, each one reducing the defects that reach end customers:
Prohan (wood panels)
Eliminated 90% of gluing defects in wooden board production and cut customer returns close to zero.
10beauty (precision robotics)
Computer vision guiding an automated manicure robot to 250 microns (0.25mm) of accuracy.
OkKast (precast concrete)
DAC’s own quality-inspection product for precast concrete blocks, verifying dimensions to roughly 1mm accuracy when scans are combined, and expanding to rebar and embedded-element positioning.
How we build your computer vision system
We don’t build blind. Every project starts with an Industrial AI workshop where we map your production line, define the problem precisely, and scope how computer vision and AI systems will fit the line and what visual data is available. You leave with a tailored quote and roadmap before either of us commits to a build.
Stage 1: Industrial AI workshop
Analysis of your process, architecture and requirements. You leave with a scoped quote and a roadmap.
Stage 2: First working pilot
One use case solved end to end, e.g. identifying a specific defect on one line.
Stage 03: Full integrated solution
Multi-use-case system with MLOps and integrations into SCADA/MES/ERP.
After go-live, we typically continue working with clients on optimisation, new features and scaling to additional lines, so the system keeps paying off as your needs change. Because every plant, dataset and integration is different, we scope and quote each stage individually rather than publishing fixed prices.
Is computer vision the right investment for your factory?
| Good fit if… | Not a good fit (yet) if… |
|---|---|
| You have, or can quickly gather, enough real examples of the defect or condition to train a model on. | Defects are too rare or too random to build a reliable dataset from. |
| Your product or environment is stable enough for repeatable measurements. | Products or processes change so often that a camera setup can’t keep pace. |
| The cost of inspection errors (returns, rework, safety incidents, lost contracts) is high enough to justify the investment. | The line runs short, ever-changing batches where manual checks are already cheap enough. |
| Your team is ready to adjust workflows around the system’s outputs. | The organisation isn’t ready to change processes or behaviour to support the system. |


If this sounds like your line, the next step is a free Industrial AI workshop.

What our computer vision systems can measure

Length, width, height, thickness, gap size, geometric tolerances, surface profile.
Deviation from CAD reference models, contour irregularities, warping.
Scratches, dents, pitting, cracks, inclusions, corrosion, coating defects.
Paint uniformity, gloss, staining, grain structure, weld and solder quality.
Missing components, incorrect orientation, incorrect labelling.
Barcodes, QR codes, serial numbers and batch IDs for traceability.
Foreign objects, worker presence in restricted zones, PPE use.
Captured with 2D cameras, multi-view 2D rigs, 3D scanners, thermal cameras, hyperspectral systems, X-ray units, polarization cameras or microscope vision, depending on what the use case needs. Getting this choice right is one of the main drivers of project success and cost.
Built to fit your existing engineering and production stack
Our computer vision systems are built on TensorFlow, PyTorch, OpenCV and ONNX, deployed to the edge on Nvidia Jetson or Coral where latency matters, and run in production with MLOps tooling (MLflow, ClearML, Weights & Biases) on AWS, GCP or Azure.
If quality problems trace back further upstream, to a drawing, a quote or a nesting decision, pair this system with our AI for technical drawings and CAD file analysis to catch issues before a part is even cut, not just after.
Machine Learning & AI


Scikit-Learn, OpenAI API, OpenMMLab, OpenVINO, Safetensors, SAM2, DINO, OpenCV, Open3D
MLOps


Weights and Biases, neptune.ai, SIGOPT, Optuna
Cloud & Data Platforms



Apache Kafka, Apache Spark, Snowflake, dbt, Argo Workflows, Matillion, Airflow, AWS Sagemaker
Data Analytics


Scikit-Learn, Polars, Prometheus, Grafana, PowerBI, Sweetviz, Seaborn
Explainable AI


LIME, ELI5, omniXAI
Data Management


PyTorch Lightning, MongoDB, Redis, MySQL, PostgreSQL, MS SQL Server, Talend, DWH & Data Lakes, Databricks, Azure Blob Storage, CVAT
Edge ML


Nvidia TAO, Edge Impulse, PyTorch mobile, Embedded systems integration
Who we build computer vision systems for
Manufacturers

Manufacturers who need a custom system fully tailored to their plant floor, not an off-the-shelf tool retrofitted to fit.
Producers
of Camera and Vision Systems

Those who need a development partner to make their hardware scalable.
Integrators
of Manufacturing Systems

Manufacturing integrators who need a partner to help their combined systems stay competitive.


Subscribe our Newsletter
Anything else we should know?
Optional, and you are already subscribed. It only helps us write for the right reader.
You are on the list.
The next one lands in your inbox. Nothing else — we do not pass your address on.
FAQ
Computer vision in manufacturing is the branch of artificial intelligence that lets cameras and machine learning models interpret video data the way a trained inspector would. A manufacturing computer vision system captures footage on the assembly line or at an inspection station, processes it with computer vision models built on machine learning algorithms, and turns the result into a decision, for example flagging a defect or confirming a part is assembled correctly. This computer vision technology now shows up across the manufacturing industry: quality control, safety monitoring, object identification and robotics are the four most common computer vision applications across manufacturing plants.
Integrating computer vision rarely means installing one isolated camera. In most manufacturing environments, the system sits alongside existing manufacturing processes and production processes, feeding data into the same systems that already run the plant (SCADA, MES, ERP), so a defect flagged by a camera can trigger an action elsewhere in the line without anyone re-entering it manually. On the assembly line itself, computer vision typically automates one manufacturing task at a time (a visual check, a barcode read, a robot’s grip position) rather than the whole process at once. That is what’s enabling manufacturers to add industrial automation gradually instead of replacing an entire line in one project. The goal at every stage is the same: optimize processes by removing a manual, error-prone step. That combination of process optimization and seamless integration with what’s already running is what turns a one-off pilot into a system that actually improves manufacturing operations day to day.
Three benefits come up most often when manufacturers describe why they invested in computer vision. First, product quality: consistent, repeatable inspection helps maintain quality standards across shifts and sites, something manual sampling alone struggles to guarantee. Second, worker safety: computer vision can enhance worker safety by watching for PPE compliance and unsafe movement in real time, a critical concern on any factory floor with moving equipment or industrial robots nearby. Third, operational efficiency: process monitoring and equipment monitoring enable real time monitoring of the line, so real time insights about a stalled process or a drifting machine reach a supervisor in seconds rather than at the next shift handover. Together, enhancing efficiency and quality standards on these manufacturing tasks tends to deliver the clearest return.
Usually not, and it shouldn’t try to. Human inspectors get tired, and subtle defects can slip past human inspectors after a few hours on the same repetitive task, a well-documented source of human error in manual quality control. Computer vision does not get tired the same way and holds its attention on hour eight as well as it did on hour one, but it also does not have human capabilities like judgment on an ambiguous edge case, or the human expertise that recognises a new failure mode nobody trained the model on. In most of our projects, the system takes over repetitive screening so human workers can focus on exactly those judgment calls instead of staring at parts all day.
It can, indirectly. The same cameras and sensors used for quality control often feed data that supports predictive maintenance, for example spotting early wear, misalignment or overheating on equipment before it causes a breakdown. Catching defects and process drift earlier also improves resource efficiency: less material is scrapped, less energy goes into reworking or re-running a batch, and machines run closer to their intended settings. For manufacturers reporting against global sustainability goals, that combination of lower waste and better energy efficiency is increasingly part of the business case, alongside the more immediate gains in quality and safety. It will not replace a dedicated energy management system, but it does reduce the energy consumption tied to rework and downtime.
It depends too much on your hardware, data and scope to quote in general terms, so we don’t publish a fixed price list. Every project starts with an Industrial AI workshop, typically a matter of days to schedule and run, where we analyse your production line and requirements and give you a tailored quote and roadmap. To get the most out of that first conversation, come with sample images or footage of both correct and defective products, access to your production team, and clarity on which system (SCADA, MES, ERP) the result needs to feed into. After the workshop, a first working pilot for a single use case typically ships in weeks rather than months, and a fully integrated, multi-use-case solution gets scoped individually once the pilot proves out.
Tell us What You Need. We Will Estimate the Solution.
Contact us!
Send us an email: [email protected]